Standardized Reman Workflows Full Quality Control System
Introduction
Quality control is the backbone of professional heavy‑duty truck remanufacturing. Unlike casual repair or cosmetic refurbishment that depends heavily on individual technician experience, a full‑set QC system builds fixed checkpoints throughout the entire standardized reman workflows, from incoming core receiving to final delivery.
Every procedure gets measurable pass‑fail criteria, records and traceable documents. This article explains how a closed‑loop full quality‑control system eliminates random quality risks and stabilizes output performance for standardized remanufacturing.
Incoming Core QC: Raw Material Gatekeeping for Reman Products
The quality of finished reman products starts with screening qualified used cores. This first checkpoint filters out unrepairable units before any disassembly work begins.
- Visual & dimensional preliminary inspection: Frame crack check, corrosion thickness measurement, deformation detection for cab, axle housings and engine blocks. Cores with fatal structural damage are directly rejected.
- Non‑destructive testing (NDT) for key load‑bearing parts: Ultrasonic testing, magnetic particle inspection to detect invisible internal cracks and metal fatigue that cannot be seen by naked eyes.
- Core grading & filing: Classify qualified cores according to damage degree, record serial number, mileage and original working condition; isolate scrapped cores to prevent them from entering subsequent production.
- Rejection rule execution: Any core exceeding fatigue threshold will not be accepted for reman, even for cost‑reduction purposes.
Disassembly QC: Condition Assessment Part‑by‑Part
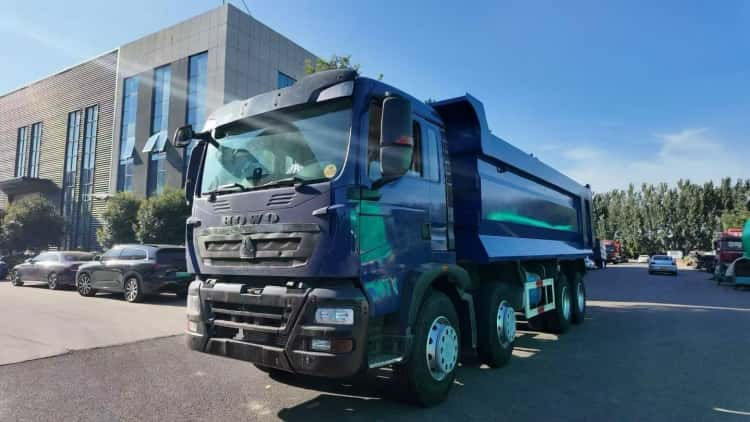
During full disassembly, QC inspectors evaluate every single component, separating scrap, repairable and directly‑reusable parts.
- One‑by‑one component tagging: Each disassembled part is marked with corresponding core serial number to maintain full traceability.
- Functional damage assessment: Check wear, clearance, thread condition, sealing surface damage for engine, gearbox, brake and chassis components.
- Three‑way sorting mechanism: Scrapped parts go to waste processing; repairable parts enter machining station; qualified reusable parts move to cleaning workshop.
- Deviation record: Abnormal wear or hidden defects are logged, feeding data back for future core‑selection optimization.
Cleaning & Machining QC: Control Precision of Repaired Components
Cleanliness and machining accuracy directly decide later assembly reliability. This link avoids hidden trouble caused by residual dirt or over‑tolerance processing.
- Cleaning effect verification: Oil, carbon deposit and rust residue must meet cleanliness standard; re‑clean is required if residues remain on metal surfaces.
- Machining dimension inspection: Crankshaft grinding, cylinder boring, bushing pressing all follow fixed tolerance ranges. Components out of tolerance must be scrapped instead of forced assembly.
- Surface hardness & material check for repaired parts: Ensure post‑machined parts keep original mechanical performance; low‑grade substitute materials are forbidden.
- Batch sampling inspection: Random spot‑check on finished machined components to avoid consistent errors from machine‑tool drift.
Parts Sourcing & Replacement QC: Control Quality of New Spares
Unqualified replacement spare parts are one major cause of reman product early failure. Strict QC covers all incoming new components.
- Supplier qualification audit: New parts shall be OEM or equivalent certified alternatives; unknown uncertified aftermarket spares are blocked.
- Incoming inspection for purchased parts: Check part number, appearance, packaging, certification documents for bearings, seals, brake components, gaskets and hoses.
- Mandatory replacement list execution: Safety‑related consumable parts cannot be reused; inspectors verify these items are fully replaced before assembly.
- Non‑conforming part isolation: Unqualified purchased spares are marked and segregated, preventing accidental mixing into assembly lines.
Assembly Process QC: Standardized Operation & Mid‑Process Check
Assembly cannot purely rely on mechanic experience; QC sets multiple intermediate checkpoints during assembly.
- SOP‑driven assembly: Enforce standard torque values, installation sequence and clearance parameters for every key joint.
- Key‑station stop‑and‑inspect mode: After engine assembling, axle assembling and brake piping installation, QC inspectors sign off before workflow moves forward.
- Real‑time operation record: Record torque data, part batch numbers and inspector initials for critical connections.
- Rework management: Mis‑assembled units go through full disassembly‑recheck procedure; rework events are logged for process review.
Post‑Assembly Bench & Vehicle‑Level Performance Testing
All reman products must pass objective performance testing, rather than only visual appearance check.
- Component bench test: Engine dynamometer test, gearbox shift test, brake‑system pressure test, hydraulic leak test for core assemblies.
- Complete vehicle functional test: Full‑system check of power output, braking efficiency, steering function, electric circuit, instrument display and emission status.
- Quantifiable pass‑fail indicators: Power, oil pressure, brake response time, noise level have clear thresholds. Units failing any index must go back for troubleshooting.
- Test‑data archiving: Store all test reports linked to vehicle serial number for future traceability.
Pre‑Delivery Final QC & Document Compliance
Before shipment, final QC confirms both physical vehicle and complete supporting documents.
- Comprehensive visual inspection: Check painting quality, cab fitting, pipeline layout, fastener locking status.
- Full‑set document verification: Reman certificate, replaced‑parts list, NDT records, bench‑test reports shall be complete and consistent.
- Random sampling audit: Small‑proportion finished‑unit re‑inspection by independent QC staff to spot procedural loopholes.
- Labeling: Paste reman identification label with unique serial number, grade and warranty information on the vehicle.
After‑Delivery Closed‑Loop QC Feedback
Quality control does not end at delivery. In‑service feedback improves the whole standardized reman workflows continuously.
- Field failure information collection: Record failure mode, component serial number and working condition for vehicles under warranty.
- Root‑cause analysis: Distinguish failures caused by core defect, spare‑part quality, assembly error or improper customer operation.
- Process corrective actions: When repeated quality issues appear, update core‑screening rules, tighten machining tolerance or adjust supplier standards.
- Periodic QC‑system review: Summarize failure data each quarter, optimize inspection checklists and update SOP for standardized remanufacturing.
Conclusion
A full quality‑control system turns reman workflows from experience‑based repair into standardized industrial production. Checkpoints cover core intake, disassembly, machining, spare‑part admission, assembly, performance testing, pre‑delivery audit and post‑sales feedback, forming a closed‑loop management.
For fleet buyers, this mature QC framework greatly reduces quality fluctuation of reman products, delivering stable reliability and transparent traceable records.
2 Comments