Reman Certification & Testing Rules for Heavy Vehicles Remanufacturing
Introduction
Testing and certification constitute the objective technical boundary separating genuine heavy reman trucks from cosmetic refurbishment or partial overhaul. Many market participants confuse superficial painting, component minor repair and basic road check with formal reman validation. Without standardized test procedures and traceable certification documents, buyers cannot verify whether a heavy reman truck reaches performance benchmarks close to original‑new specification.
Complete reman testing runs through incoming core screening, component‑level inspection, sub‑assembly bench validation, finished‑vehicle comprehensive test and final third‑party certification. reman certification is not merely a paper certificate; it represents full compliance with workflow rules, measurable test data and auditable quality evidence, forming the fundamental basis for cross‑border trade, fleet asset valuation, warranty execution and ESG compliance.
Core‑Unit Incoming Inspection Rules (Pre‑Production Gatekeeper)
The quality of incoming core chassis, frame and powertrain assemblies determines the upper limit of final reman output. Strict incoming testing eliminates cores with irreparable structural damage before reman workflows start.
- Frame and load‑bearing structure non‑destructive testing: Apply NDT inspection for frame cracks, weld fatigue and deformation. Any core with penetrating crack, permanent bending beyond allowable tolerance or major collision damage shall be rejected and cannot enter reman production.
- Powertrain baseline evaluation: Record original compression pressure, oil leakage status, wear clearance of engine, gearbox and axle before disassembly, used as reference benchmark for post‑remanufacturing performance comparison.
- Component grading rule: Classify incoming cores into reman‑eligible, repairable and scrap grades according to unified tolerance thresholds. Scrapped assemblies cannot be reused by simple welding or surface repair.
- Document requirement: All incoming inspection results, NDT reports and core grading records must be archived into traceability system, rather than relying on manual visual judgement only.
Component‑Level Testing After Disassembly & Cleaning
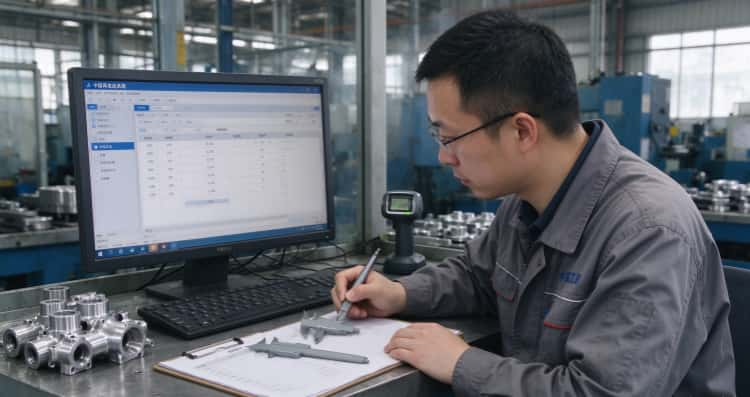
After full disassembly and precision cleaning, every key component goes through dimensional measurement and defect detection. This phase differentiates remanufacturing from simple overhaul which skips granular component validation.
- Dimensional tolerance measurement: Measure shaft run‑out, gear tooth wear, cylinder bore tolerance, bearing seating surface deformation. Parts exceeding allowable machining tolerance shall be scrapped instead of forced assembly.
- Mandatory safety‑related component screening: Brake assemblies, sealing kits, rubber hoses, bearings and fasteners are subject to 100‑percent inspection; aging safety components must be replaced instead of repaired.
- Repaired‑part validation: For components restored by machining, welding or surface treatment, secondary inspection is required to confirm mechanical performance meets specification before reassembly.
- Scrap record keeping: Record serial numbers and scrap reasons for all discarded critical parts for audit traceability.
Sub‑Assembly Bench Test Standards
Bench testing validates powertrain and key assemblies under controlled laboratory conditions, independent of vehicle road status. Bench test data serves as objective quantitative proof for reman performance.
- Engine bench test items: Rated power output, torque curve, cylinder compression balance, fuel consumption under standard working condition, exhaust emission index, oil pressure stability, no‑load and full‑load leakage check. Engine performance shall reach the original new‑product specification range.
- Gearbox and axle bench validation: Shift smoothness, load‑bearing noise detection, gear meshing status, oil seal leakage test under simulated load condition.
- Brake system bench calibration: Air pressure build‑up speed, brake response time, pressure holding performance, air circuit tightness test for the whole brake assembly.
- Pass‑fail rule: Any sub‑assembly failing bench test must be disassembled and reworked; no defective unit can move forward to vehicle assembly. All bench‑test curve data shall be saved within reman traceability archive.
Finished‑Vehicle Integrated Testing Rules
After full reassembly is completed, the whole heavy reman trucks carries out static inspection and dynamic road test to verify coordination performance of all systems.
- Static finished‑vehicle inspection: Whole‑vehicle circuit detection, pipeline layout inspection, fluid filling verification, sealing check for all joint positions, warning‑light self‑check of instrument panel.
- Loaded road test cycle: Include start‑stop, acceleration‑deceleration, climbing simulation, emergency braking, steering stability, high‑speed cruising and low‑speed heavy‑load running. Monitor abnormal noise, oil‑water leakage, brake performance and temperature rise of key assemblies.
- Post‑road‑test re‑inspection: After road test completes, re‑check all sealing positions, fastener torque and fluid status. Resolve all abnormal items before final delivery.
- Test‑data archiving: Record road‑test mileage, fault codes, abnormal phenomena and rectification records, attached to each vehicle’s unique traceability ID.
Factory Internal Certification Requirements
Internal factory certification represents self‑compliance verification of remanufacturer, but cannot replace independent third‑party audit.
- Quality‑system baseline: Remanufacturer shall operate under ISO 9001 quality‑management system, follow unified reman workflow specification.
- Internal QC final sign‑off: Authorized quality engineers review full‑process records: incoming core report, component inspection log, bench‑test data, finished‑vehicle road‑test result. Only vehicles passing all items can obtain internal reman release certification.
- Mandatory content of internal reman certificate: Unique reman asset ID, original VIN information, production completion date, scope of replaced key components, factory test summary, warranty start‑time and coverage statement.
- Limitation: Factory‑self‑issued documents are not sufficient for cross‑border high‑value fleet procurement, which requires independent third‑party verification.
Third‑Party Independent Audit & External Certification Rules
Third‑party reman certification delivers neutral credibility for cross‑border buyers, solving trust risks brought by factory self‑declaration.
- Audit scope: Third‑party institutions verify whether remanufacturer follows standard workflow, spot‑check NDT records, bench‑test reports, component replacement list and finished‑vehicle test result; may conduct physical sampling inspection on finished reman trucks.
- Valid deliverables: Third‑party reman compliance report, key‑assembly inspection certificate, pre‑shipment inspection report issued by qualified independent organization.
- What genuine third‑party certification cannot do: It cannot simply re‑print supplier‑provided data without independent on‑site verification. Photos of vehicle appearance or paint effect do not count as reman certification.
- Cross‑border practical value: Third‑party documents support import customs review, fleet tender submission, financing asset assessment and warranty dispute arbitration.
Distinguish Valid Reman Certification from Misleading Market Documents
Many traders produce decorative certificates for refurbished trucks, which lack technical test support. Buyers need to identify invalid pseudo‑certification.
- ❌ Pseudo‑certificate 1: Simple decorative reman certification without attached underlying test data.
- ❌ Pseudo‑certificate 2: Only before‑and‑after renovation photos, no NDT, bench‑test or road‑test quantitative indicators.
- ❌ Pseudo‑certificate 3: General‑format used‑vehicle inspection report, which only checks appearance and basic start‑up status, not reman‑specific full‑disassembly and performance‑restoration validation.
- ✅ Valid reman certification package includes: core incoming NDT report, key‑component inspection log, powertrain bench‑test curve record, finished‑vehicle road‑test summary, internal release document plus optional third‑party audit report, linked to unique traceability ID.
Common Gaps and Industry Limitations of Global Reman Testing‑Certification System
Although standardized reman testing and certification are critical pillars, global industry still faces structural obstacles.
- Regional standard divergence: Different countries hold different reman definition and acceptance thresholds. There is no single unified global reman certification standard, increasing cross‑border compliance workload.
- Implementation gap: Some workshops adopt simplified reman testing workflows; only carry out partial‑item inspection rather than full‑process validation, while issuing self‑claimed reman certificates.
- Third‑party capacity imbalance: In some supply regions, qualified institutions capable of professional heavy‑vehicle reman audit are insufficient. Many inspection agencies only execute used‑vehicle condition check instead of reman‑oriented technical audit.
- Future direction: Industry pushes for mutual‑recognition framework for reman testing specifications, and links reman certification documents with digital traceability system to prevent certificate forgery and reuse.
Conclusion
Reman testing and certification form the technical baseline of certified heavy reman trucks. Complete validation covers incoming‑core NDT screening, component‑level inspection, sub‑assembly bench testing, finished‑vehicle road test, internal factory release and independent third‑party audit.
Certification is not isolated paper output; it must bind with complete measurable test data and full‑lifecycle traceability archive. Genuine reman cannot be proved merely by vehicle appearance, paint quality or simple startup check. For global fleet buyers, verifying complete testing‑certification document packages is the core method to filter out fake‑reman refurbished products, control procurement risk and guarantee long‑term asset performance.